Industrial fixtures and jigs
Glass-Filled Nylon SLS for Industrial Fixtures and Jigs
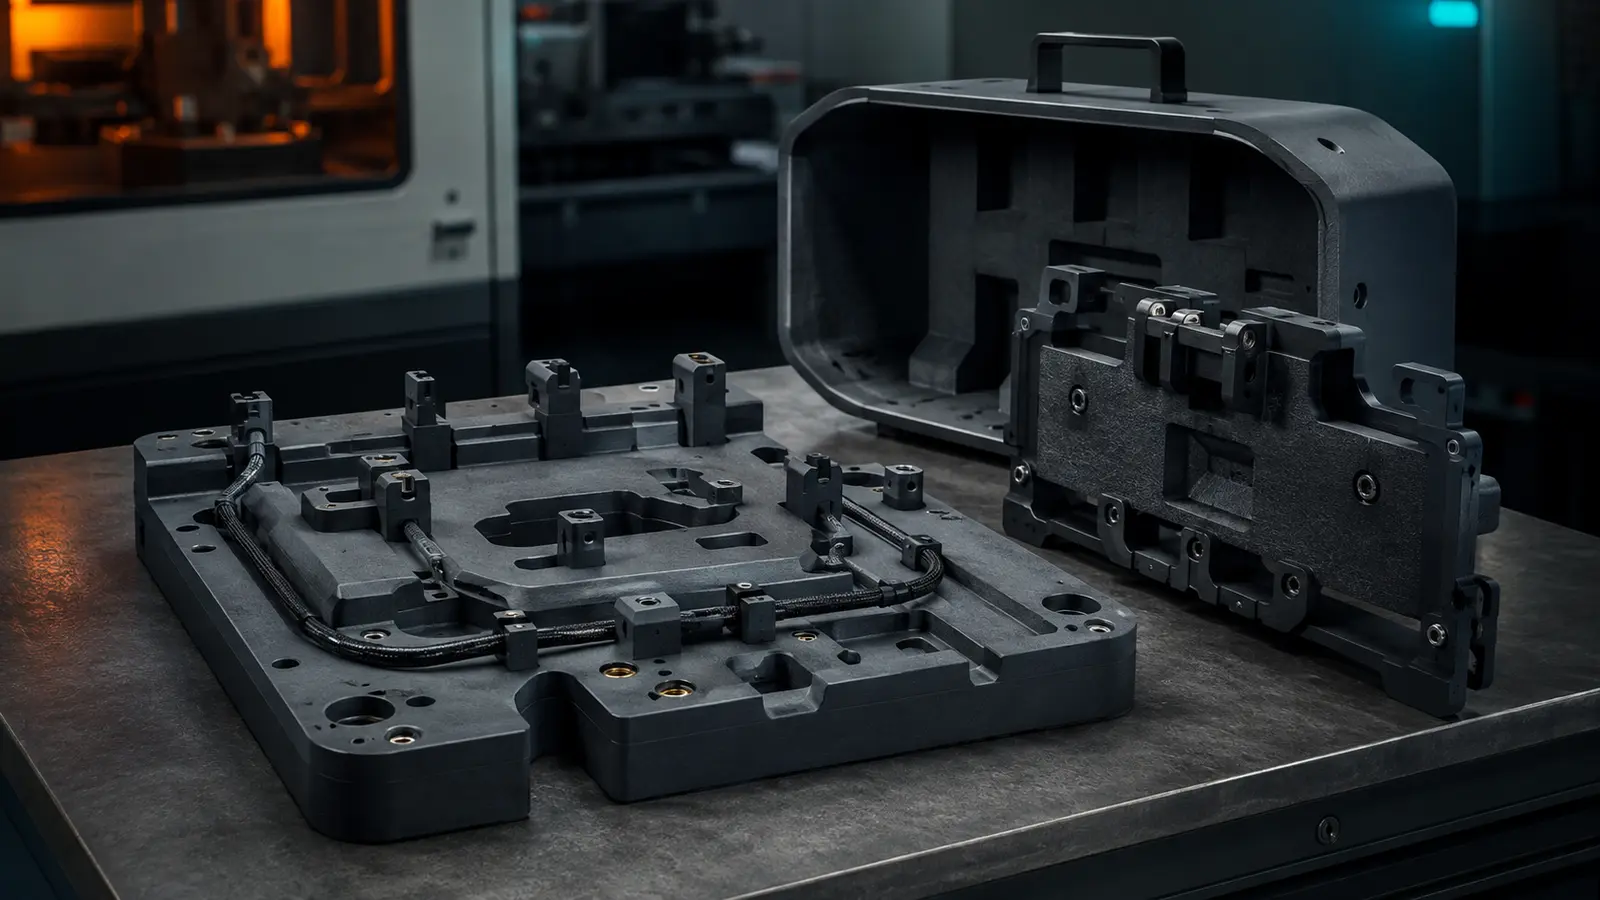
Build rigid jigs, fixture bases, inspection tools and machine covers without tooling, using PA12GB or PA12 based on stiffness, load and assembly needs.
Target customers
Industry pain points
What makes this application difficult?
- !Factory-floor jigs often need quick changes after operators test real workflows.
- !CNC fixtures can be expensive for low-volume or geometry-rich production aids.
- !Rigid bases, inspection tools and machine covers need better flatness and screw-zone design than ordinary prototypes.
SLS solution
How SLS helps before tooling
- ✓SLS makes it practical to build custom jigs, nests, covers and tool holders in low volume.
- ✓PA12GB offers higher stiffness for fixture bodies, while PA12 remains useful for balanced functional parts.
- ✓DFM review checks wall thickness, insert bosses, datum surfaces and post-processing effects before production.
Application modules
Parts commonly reviewed for Industrial Fixtures
Use these examples to prepare CAD files, quantities and critical-feature notes for RFQ review.
Assembly jigs and fixtures
Inspection nests and gauges
Machine covers and guards
Tool holders and trays
Positioning blocks and bases
Robot cell fixture parts
Drill and marking templates
Low-volume factory aids
Material recommendation
Choose PA12, PA11, PA12GB or TPU by function
Material choice should follow the real load case: stiffness, impact resistance, repeated flexing, contact feel and finishing requirements.
Case module
Problem-material-quantity-cycle-result format
This de-identified pattern shows the kind of project information that makes DFM review and quotation more accurate.
Design advice
DFM notes before uploading CAD
Use PA12GB when fixture rigidity and flatness matter more than snap-fit behavior.
Add ribs and fillets around tall bosses, screw zones and fixture datum areas.
Specify which surfaces are locating or inspection-critical so they can be reviewed separately.
Use threaded inserts for repeated assembly or fixture maintenance points.
Account for post-processing and dyeing where fixture parts contact production components.
Related engineering resources